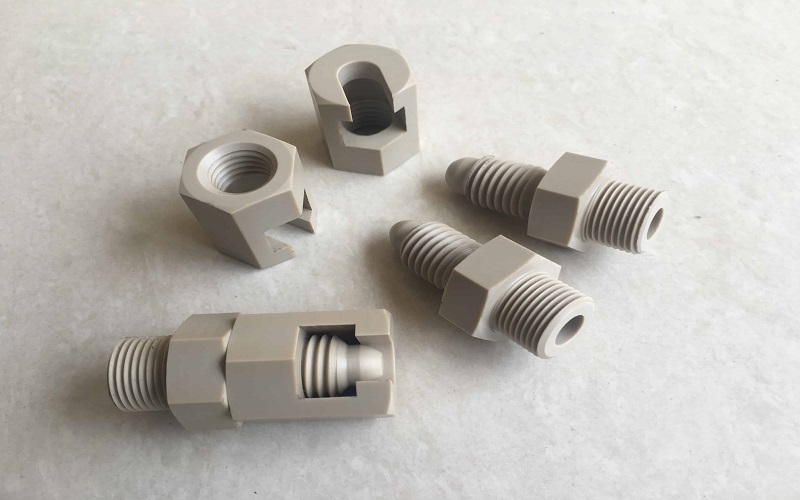
The realm of high-performance polymers is always expanding. Polymers that were earlier obscure (and therefore prohibitively expensive) slowly discover use cases in critical (read: price-insensitive) industries, gradually reaching a critical mass of volume beyond which commercial usability becomes more apparent. PAI is one such polymer.
Few in the family of high-performance polymers have a position as commanding as polyamide-imide (PAI), sold most widely under the trade name of Torlon®. It has the unique distinction of being the strongest thermoplastic that is still melt-processable. It retains that strength at temperatures where most engineering plastics have long since softened. It is this combination of metal-like performance with the design freedom of a moulding process that makes PAI the material of choice for components that have to survive punishing thermal, mechanical, and chemical loads.
The features that differentiate PAI
PAI is an amorphous polymer with a glass transition temperature around 280°C and a continuous service temperature of about 260°C. Unfilled grades provide tensile strengths of 150-190 MPa, with reinforced grades over 205 MPa—numbers similar to cast metals. Importantly, PAI retains much of this strength at elevated temperatures where materials like PEEK start to lose stiffness.
Besides its strength, PAI has excellent wear resistance, very low creep, high compressive strength, and one of the lowest coefficients of thermal expansion of any unreinforced plastic. It is also highly resistant to radiation, losing only about 5% of its tensile strength after exposure to 10⁹ rads of gamma radiation, a quality that makes it attractive for use in the nuclear and aerospace industries. Its main limitations are cost, sensitivity to strong bases and long steaming at high temperatures, and a hygroscopic nature that requires careful drying before processing.
Understanding Grades
PAI is available in a few well-defined grades, each tuned to a different balance of strength, wear, and stiffness.
Torlon® 4203: General purpose grade with the best impact resistance and elongation of the family. It's the natural starting point for structural and electrical parts that need toughness, but not extreme wear resistance.
Torlon® 4301 and 4275: Bearing and wear grades, compounded with graphite and PTFE to reduce the coefficient of friction and facilitate dry, non-lubricated running. These are the workhorses for bushings, thrust washers, wear rings and seal components.
Torlon® 5030: 30% glass-fibre reinforced, with higher stiffness and dimensional stability, while retaining good electrical insulation properties – for structural parts and housings.
Torlon® 7130: 30% carbon fibre-reinforced, with the highest stiffness and lowest thermal expansion of the range and also the electrostatic dissipative behaviour valued in semiconductor handling.

Processability: Moulding Extrusion & Machining
The difference between PAI and the very best-performing polymers is that it can be processed with conventional melt processes, but this is by no means trivial.
The principal advantage of PAI over non-melt-processable materials is that it can be injection moulded into complex near-net-shape parts. But it behaves like a reactive polymer. After moulding, parts require a long post-cure, held at increasingly higher temperatures over a number of days—longer for thick sections. During this time, the polymer chains stretch and cross-link to achieve full strength and chemical resistance. There are fewer than 100 processors in the world that can do this reliably.
Compression moulding: This method is widely used for larger or simpler shapes and for the manufacture of stock shapes. It does not suffer from some of the flow limitations of injection moulding.
Extrusion: Tubes, rods and other stock profiles are extruded and cured to give semi-finished shapes which are subsequently machined into precision parts.
Machining: Fully cured PAI stock shapes machine cleanly and hold tight tolerances, making machining the preferred method for low volumes, prototypes and highly precise components. Unfilled grades cut much like a tough engineering plastic, but glass- and carbon-filled grades are abrasive and require carbide or diamond tooling. For critical parts, a short re-cure after extensive machining restores surface properties. Moulding and machining in-house means that the process can be tailored to the volume and precision required for each project.
How PAI Stacks Up to Other High-Performance Polymers
If you put PAI against its neighbours, we can see when the premium is justified.
PEEK: Much easier to process. Semi-crystalline. No post-cure needed. PEEK is the more forgiving material but with about half the tensile strength of PAI and poorer performance at the top of the temperature range. PEEK also has better resistance to hot water and steam, whereas PAI can hydrolyse.
PTFE: A completely different beast. While PTFE has unparalleled chemical inertness and the lowest friction of any polymer, it cannot be melt-processed and has very low strength and high creep. PAI is selected exactly where PTFE fails, under steady high load and stress.
PPS: Economical, easily moulded, chemically resistant workhorse. Much weaker and more brittle than PAI. Limited to lower continuous temperatures.
PESU: Amorphous, steam-sterilisable polymer. Good hydrolysis resistance, easy to process, but poor mechanical and thermal properties compared to PAI.
PEI (Ultem): The closest amorphous cousin, a popular "no-fuss" choice, easy to mould and much cheaper, but less strong and with a lower service temperature.
Polyimide (Vespel): This is the one material that clearly outperforms PAI on temperature, but it is not melt-processable, being produced by sintering and machining at considerable cost. PAI provides near-polyimide performance with the manufacturability of a moulded thermoplastic.
Applications of PAI
PAI’s unique combination of strength, temperature resistance and wear performance make it the choice for the most demanding corners of industry.
Oil and gas: compressor valve plates, back-up rings, and seal components must withstand pressure and heat in downhole environments.
Aerospace: fasteners, bushings and bearing cages where it replaces metal and reduces weight.
Semiconductor manufacturing: Its purity, dimensional stability and electrostatic-dissipative grades are suitable for g wafer-handling components
Automotive: PAI thrust washers and seal rings are used in automotive transmissions.
In all these the common thread is a part that must act like metal but weigh less, run dry or tolerate a harsh environment.
Why PAI?
PAI is not the answer to all high-temperature problems, and the cost and processing requirements limit its use to applications where nothing else will do. But when a component needs to combine the highest mechanical strength available in a mouldable plastic with excellent wear and thermal resistance, PAI is virtually unmatched. Choosing the right grade and the appropriate mix of moulding and machining is what turns that material potential into a reliable, precision component.
Read More
1. PTFE in Brake Cables
2. Graphene in Polymers - The Way of the Future
3. Injection Moulding of PEEK and PPS